How to Choose China Chromium Carbide Overlay Plate?

Choosing a China Chromium Carbide Overlay Plate requires more than comparing advertised hardness numbers. The correct plate must match the actual wear mechanism, operating temperature, impact level, and material flow. Abrasion from sharp quartz differs greatly from sliding coal dust or repeated rock impact. A plate that performs well in a chute may fail inside a crusher. That difference matters.

Dr. Lijun Zhang, a metallurgical engineer specializing in wear-resistant materials, states, “The right overlay plate is selected by wear mechanism, not by hardness alone.” This principle should guide every purchase. Review the chromium and carbon chemistry, carbide distribution, overlay thickness, base-metal grade, and welding quality. Ask for test reports, dimensional tolerances, production records, and traceable inspection data. A reliable supplier should explain its process clearly, not hide behind impressive figures.

Inspect the working environment closely. Measure temperature, particle size, impact frequency, and replacement intervals. Confirm whether cutting, bending, or field welding will be required. Some plates offer excellent abrasion resistance but limited forming flexibility. Others crack under impact because the deposit is too hard or poorly supported. Harder is not always better. That is an easy mistake to make.

Before approving a large order, request samples or references from comparable applications. Compare service life, downtime, installation effort, and total cost. Standards help, but they cannot replace field evidence. Even experienced buyers can overlook changing feed materials or uneven wear patterns. Therefore, document the decision and review it after installation. The best China Chromium Carbide Overlay Plate is not merely the hardest option. It is the most suitable, verifiable, and consistently manufactured solution for your equipment.
How to Choose China Chromium Carbide Overlay Plate?

Define Chromium Carbide Overlay Plate and Its Wear-Resistant Structure

How to Choose China Chromium Carbide Overlay Plate?

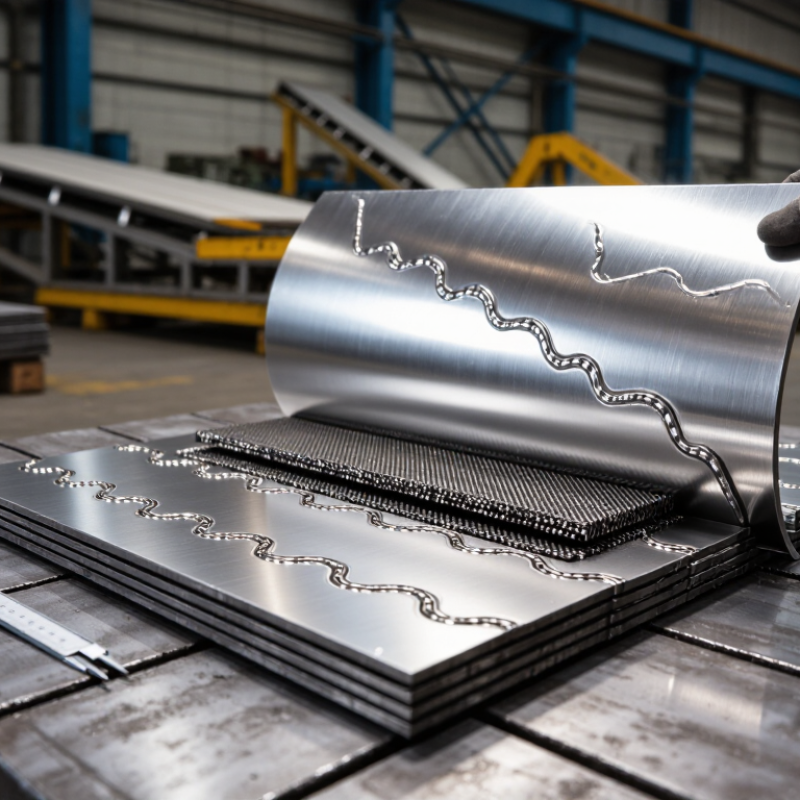
Chromium carbide overlay plate combines a tough carbon-steel backing with a hardfaced wear layer. The overlay usually contains chromium-rich carbides, mainly Cr7C3, within an iron-chromium-carbon matrix. This structure resists sliding abrasion, impact, and mineral cutting. It is not ordinary stainless steel. The backing supports welding, bolting, and controlled forming, while the carbide layer absorbs surface wear.

The USGS Mineral Commodity Summaries 2024 estimated global chromite mine production at approximately 41 million metric tons in 2023. This scale reflects chromium’s importance in alloy and wear-resistant material supply. However, chromium content alone does not prove plate quality. Buyers should request chemical analysis, carbide morphology, overlay thickness, dilution control, and crack distribution. Fine transverse cracks can relieve stress. Excessive cracks may expose the backing prematurely.

ASTM G65 testing can compare dry-sand rubber-wheel abrasion performance. It cannot fully reproduce impact from a limestone crusher or sliding coal dust. Hardness also needs careful interpretation. A very hard layer may chip under repeated impact. Practical selection should match the wear mechanism, operating temperature, particle size, and support condition. For example, a 10 mm overlay on a 6 mm backing behaves differently from the same overlay on a 12 mm backing. Plate flatness, cut-edge quality, and welding procedures deserve attention too. Many specifications still focus on hardness first, which is convenient but incomplete.

Identify Operating Conditions and Abrasion Risks

Choosing a China chromium carbide overlay plate starts with the operating conditions, not the advertised hardness. A chute handling dry iron ore faces severe sliding abrasion. A crusher feed hopper faces impact and gouging. These stresses require different plate designs.

The U.S. Geological Survey’s Mineral Commodity Summaries 2024 reported global iron ore production at approximately 2.5 billion metric tons in 2023. That volume reflects the enormous amount of abrasive material moving through equipment. Particle size, moisture, speed, and drop height can change wear patterns quickly. Fine, dry particles may polish a surface. Large rocks can crack an overlay. Temperature and corrosion also matter, especially around cement kilns and steel-processing lines.

ASTM G65 testing measures abrasive wear through volume loss, usually in cubic millimetres. It supports comparison, but it does not guarantee field life. Hardness alone can mislead. A very hard layer may resist sliding wear but fail under repeated impact. Check the base plate, overlay chemistry, crack pattern, weld direction, and recommended working temperature. Ask for traceable test reports and inspect actual worn parts when possible. My own caution is simple: laboratory data is useful, but production debris is rarely so cooperative.

Tips: Record material type, particle size, moisture, impact height, and operating temperature. Photograph worn areas before replacement. Then match the plate to the dominant wear mechanism, not a single hardness number.

How to Choose China Chromium Carbide Overlay Plate? Identify Operating Conditions and Abrasion Risks

Abrasive hardness is an important first screening factor when selecting chromium carbide overlay plate. Common abrasive materials range from coal at approximately 2–2.5 on the Mohs scale to corundum at approximately 9 and diamond at 10. Higher-hardness particles generally increase sliding and gouging wear, while impact, particle size, temperature, corrosion, and material flow rate must also be evaluated before specifying plate thickness and overlay structure.

Compare Plate Materials, Hardness, and Thickness Options

How to Choose China Chromium Carbide Overlay Plate?

Material selection starts with the abrasive, not the supplier’s headline hardness. Chromium carbide overlay plate combines a mild-steel backing with welded, chromium-rich wear layers. The backing supports bending and attachment, while the overlay resists sliding particles and impact. For severe mineral abrasion, a deposit near 55–65 HRC is common. Harder is not always wiser. Excessive hardness can increase cracking when impact loads are high.

Thickness should match both wear rate and structural demand. Typical overlay thicknesses range from 3 to 20 mm, but this range needs verification. A 6 mm layer may protect a transfer chute, while a 12 mm layer can suit a heavily loaded hopper. Measure the original wall thickness, clearance, and expected service interval. A plate that is too thick may interfere with flow or create difficult welding transitions. That mistake is easy to overlook.

Ask for test evidence, not only a hardness value. ASTM G65 Procedure A uses 6,000 wheel revolutions for controlled abrasive-wear comparison. Request mass-loss results, test conditions, deposit chemistry, and hardness mapping. ISO 6507-1 provides the Vickers hardness method, which helps compare uneven overlay surfaces. The 2024 USGS Mineral Commodity Summaries estimated global chromite mine production at roughly 41 million metric tons in 2023, showing the scale of chromium supply. Yet ore chemistry varies. I would still question any datasheet lacking dilution data, crack guidance, or thickness tolerance. Real service conditions often expose those gaps.

Evaluate Manufacturing Quality, Standards, and Supplier Capability

When choosing a China chromium carbide overlay plate, evaluate manufacturing evidence rather than relying on a polished catalogue. Confirm the base steel grade, overlay chemistry, carbide distribution, hardness range, and plate thickness. Ask for heat numbers and inspection records linked to each shipment. Demand evidence.

A reliable producer should provide clear quality procedures, calibrated hardness testers, welding procedure qualifications, and dimensional inspection data. Request abrasion results from recognized methods, such as ASTM G65, when they match your working conditions. Check whether the test sample represents the actual production plate, not a specially prepared piece. That difference matters. Examine surface cracking carefully, because controlled transverse cracks can relieve stress, while irregular cracks may indicate poor process control. Check flatness, cut-edge quality, and overlay thickness at several points. One measurement is not enough.

Supplier capability also includes practical support. The technical team should understand impact, sliding abrasion, temperature, and installation constraints. Review production capacity, lead times, cutting equipment, export packaging, and traceability systems. I have learned that certificates alone can hide weak inspection habits. A small trial order, followed by independent testing, often reveals more than a long presentation. Still, trial testing is not perfect; laboratory wear may differ from field conditions. Record failures honestly, including premature wear, warping, or welding difficulty. A capable supplier should discuss these findings without defensiveness and adjust specifications when necessary.

How to Choose China Chromium Carbide Overlay Plate? - Evaluate Manufacturing Quality, Standards, and Supplier Capability
Evaluation Category Quality Dimension Recommended Evaluation Target Verification Method or Reference Standard Documents or Records to Request
Material Composition Chromium–carbon alloy chemistry Typical chromium carbide overlay deposits use an iron–chromium–carbon system. Common commercial ranges are approximately 15–40% chromium and 3–6% carbon by mass, although the suitable range depends on the wear application. Verify by optical emission spectroscopy, X-ray fluorescence, or another calibrated chemical analysis method. Heat or batch chemical composition report, material traceability record, and independent test report when required.
Overlay Hardness Hardness of the wear-resistant deposit A typical chromium carbide overlay deposit is approximately 55–65 HRC. The specified value should be agreed according to impact, abrasion, temperature, and service conditions. Rockwell C hardness testing or converted Vickers hardness testing. Hardness conversion should follow an accepted conversion standard rather than an unsupported direct comparison. Hardness map showing test locations, test load, equipment identification, calibration status, and measured results.
Microstructure Carbide distribution and matrix uniformity The overlay should show a reasonably continuous wear layer with evenly distributed chromium-rich carbides in an iron-based matrix. Excessive porosity, unmelted particles, cracks, or large segregated areas should be investigated. Metallographic cross-section, polishing, etching, and optical microscopy. Scanning electron microscopy and EDS may be used for detailed verification. Representative micrographs from the beginning, middle, and end of production, including sample identification and magnification.
Dimensional Quality Base plate thickness and overlay thickness Common overlay thicknesses are approximately 3–12 mm, with base plate thickness selected for structural strength and installation requirements. Actual tolerances must be stated on the purchase specification. Calibrated ultrasonic thickness gauge, micrometer, vernier caliper, or destructive cross-section measurement. Dimensional inspection report with a measurement grid, nominal dimensions, tolerance limits, and sampling plan.
Surface Condition Flatness, edge condition, and visible defects The plate should be free from unacceptable delamination, deep undercutting, excessive spatter, sharp untrimmed edges, and areas without required overlay. Controlled stress-relief cracks may be acceptable in some hardfacing designs, but this must be agreed in advance. Visual inspection, straightedge or digital flatness measurement, and liquid penetrant testing where crack acceptance criteria require it. Visual inspection checklist, defect photographs, flatness results, repair records, and approved sample or acceptance standard.
Wear Performance Abrasive wear resistance Performance should be compared using the same test conditions. A lower mass loss indicates better resistance in a two-body or three-body abrasion comparison; no universal value should be accepted without defining the test parameters. ASTM G65 dry sand/rubber wheel abrasion test or an application-specific comparative test. Test load, wheel speed, abrasive type, and duration must be reported. Complete wear-test report including specimen preparation, test parameters, initial and final mass, mass loss, and repeatability data.
Welding and Bond Integrity Fusion between overlay and base plate The overlay should be metallurgically bonded to the base plate without unacceptable lack of fusion or continuous separation. Weld procedure controls should address heat input, preheating, interpass temperature, and distortion. Cross-sectional macro examination, ultrasonic testing where suitable, and review of welding procedure qualification records. Welding procedure specification, welder qualification records, heat-input logs, non-destructive test reports, and repair history.
Quality Management Process control and inspection system A capable manufacturer should maintain documented control of incoming materials, welding parameters, calibration, nonconforming products, corrective actions, and final release inspection. Supplier audit against ISO 9001-based quality management practices and review of actual production records. Valid quality-management certificate, internal audit summary, calibration register, inspection and test plan, and corrective-action records.
Standards Compliance Applicable technical standards The supplier should clearly identify which requirements are contractual and which are reference methods. ASTM G65 is commonly used for abrasion testing; ASTM E384 or ISO 6507 may be used for microhardness; chemical and dimensional requirements should be defined in the purchase specification. Check the latest applicable edition of each standard and confirm that the supplier's test method, equipment, and reporting format match the agreed requirement. Standards compliance matrix, test procedures, equipment calibration certificates, and third-party inspection records where specified.
Supplier Capability Production capacity and technical support The supplier should demonstrate stable capacity for the required plate size, thickness, overlay method, production volume, cutting, forming, and repair requirements. Technical support should include installation guidance and service-condition recommendations. Factory audit, sample-order review, production-capacity assessment, and evaluation of reference projects in comparable wear applications. Production-flow chart, equipment list, capacity statement, inspection staffing plan, sample approval records, and warranty terms.
Traceability and Delivery Batch identification and documentation completeness Each plate or production batch should be traceable to base material, welding consumables, production date, inspection results, and final packing information. Review marking, packing-list information, material certificates, inspection records, and document-control procedures. Mill certificate, batch number, inspection certificate, packing list, certificate of conformity, and shipment photographs.
Note: The values shown are practical reference ranges for preliminary supplier screening, not universal acceptance limits. Final requirements should be established from the operating temperature, abrasive material, impact level, plate geometry, welding procedure, and applicable contract standard.

Select the Best Plate for Installation, Maintenance, and Cost Control

Choosing a China chromium carbide overlay plate should begin with the duty, not the advertised hardness. The USGS Mineral Commodity Summaries 2024 reported approximately 41 million metric tons of chromite ore production in 2023. The World Steel Association recorded about 1.89 billion tonnes of crude steel production that year. These figures show a large industrial supply chain, but they do not guarantee equal plate quality.

Installation details decide early performance. Measure impact, sliding abrasion, temperature, and material size at the transfer point. Specify overlay thickness, base-plate grade, crack pattern, and flatness. ASTM G65 testing can compare abrasive wear resistance under controlled conditions. It cannot predict every conveyor or chute result. Leave clearance around bolt holes. Avoid forcing a rigid plate onto a curved shell. It may crack.

Maintenance should be planned before delivery. Keep spare pieces for high-wear corners, and record plate thickness during each shutdown. A simple inspection log can reveal uneven feed or poor alignment. Harder is not always better. Excessive hardness may reduce cutting resistance but increase chipping under heavy impact. The lowest purchase price can become expensive after repeated welding, downtime, and transport. Calculate cost per operating hour, not cost per square metre. I would also question laboratory data without test conditions, sample location, and independent verification. That caution is easy to overlook.